

Post Summary
What is a Maintenance Level?
Level one maintenance is the simplest tier of maintenance work: routine, low-risk tasks performed on easily accessible parts by the equipment operator or a non-specialist employee, with no disassembly and no diagnosis required. Lubrication, visual inspection, filter and bulb changes, fluid top-offs, and condition checks are level one tasks. The five-level scale comes from the French standard AFNOR NF X 60-000 (formerly X 60-010) and rises to level five, which only the manufacturer can perform.
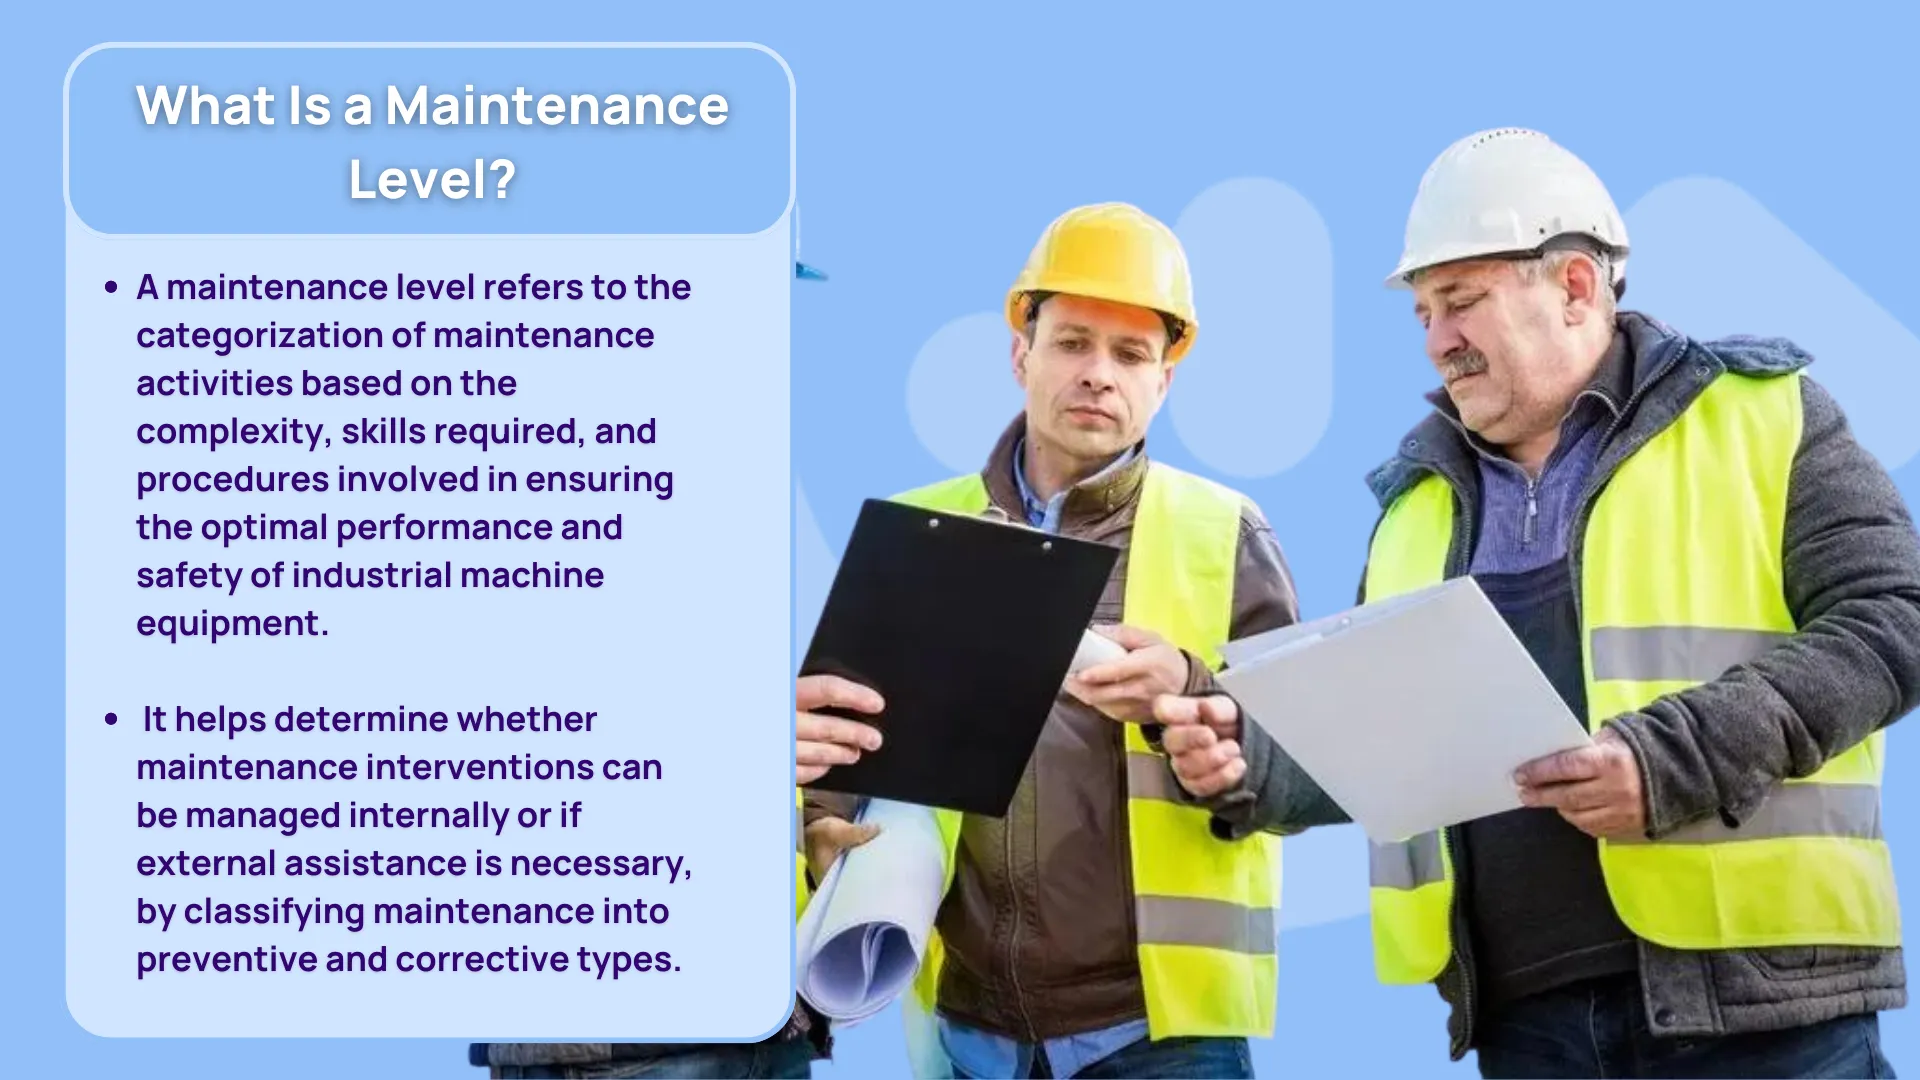
A maintenance level tells you two things fast: what skill the job needs, and whether your own people can do it. The goal of maintenance levels is to keep industrial machine equipment running safely and productively at the lowest sensible cost. The same scale works just as well on a fryer, a fuel dispenser, or a rooftop HVAC unit. It also settles the question every ops leader asks at some point: do we fix this in-house, or does this become a vendor call?
The scale is not folklore. It comes from AFNOR NF X 60-000, which replaced the 1994 X 60-010 standard and defines five levels by intervention complexity, with level one covering "simple interventions, necessary and carried out on easily accessible elements" performed by operators or non-specialized staff. The AFNOR standard record for NF X60-000 is the primary reference. The companion terminology standard, BS EN 13306:2017, splits all maintenance into preventive and corrective, with preventive further divided into predetermined and condition-based work. The degree of expertise required rises as you climb the complexity scale, which is exactly how preventive and corrective work get sorted.
The five maintenance levels at a glance
| Level | Who performs it | What it involves | Tools and parts | Multi-unit example |
|---|---|---|---|---|
| 1 | Equipment operator or store-level staff, no specialist training | Routine checks on accessible parts. No opening, no disassembly, no diagnosis | Basic hand tools and consumables such as bulbs, oil, filters, cleaner | Kitchen team wipes and checks the fryer filter and logs the walk-in temp on the opening checklist |
| 2 | Trained technician or a trained operator following a written procedure | Simple part swaps and adjustments with documented steps, no major disassembly | Spare belts, fuses, filters, plus a work order system | Store tech swaps a cooler door gasket or a hood filter on a scheduled PM |
| 3 | Specialized technician | Diagnosis before repair. Partial disassembly. Interpretation of readings | Measuring instruments, schematics, parts inventory | Refrigeration vendor traces and repairs a refrigerant leak on a walk-in |
| 4 | Certified specialist team, usually supervised, often in a workshop | Major repair, overhaul, alignment, vibration and thermography work | Dedicated workshop and advanced diagnostics | Compressor valve replacement or dynamic balancing on rooftop HVAC |
| 5 | The OEM or an OEM-authorized shop | Rebuild, remanufacture, structural restoration, design modification | Factory-grade tooling and conditions | Fuel dispenser remanufacture or a full ice machine rebuild by the manufacturer |
Three different things get called "maintenance levels"
Searchers land on this term from three directions. Knowing which one you mean prevents a lot of wasted argument in a planning meeting.
AFNOR complexity levels 1 to 5. Levels defined by how hard the job is and how much skill it needs. This is the dominant sense in industrial, facilities, and European maintenance writing, and it is the one used throughout this article.
US federal echelon levels. Defense, aviation, and government readers use organizational, intermediate, and depot instead of numbers. Per 22 CFR 120.45, organizational-level maintenance is "the first level of maintenance that can be performed on-equipment... without specialized training. It consists of repairing, inspecting, servicing, calibrating, lubricating, or adjusting equipment, as well as replacing minor parts, components, assemblies, and line-replaceable spares or units." Intermediate-level work happens off-equipment at designated shops or field teams. Depot-level work is a major repair facility rebuild. In plain terms, organizational-level maintenance is the federal-regulation name for level one maintenance. The Marine Corps maps the same three categories to five echelons in MCWP 4-11.4, Maintenance Operations.
TPM autonomous maintenance (jishu hozen). The lean-manufacturing sense. Level one maintenance is the task list. Autonomous maintenance is the program that hands those tasks to operators and makes them stick, in seven steps starting with an initial clean and inspect. If your team runs a total productive maintenance program, level one is the work you are transferring.
Preventative Maintenance Levels
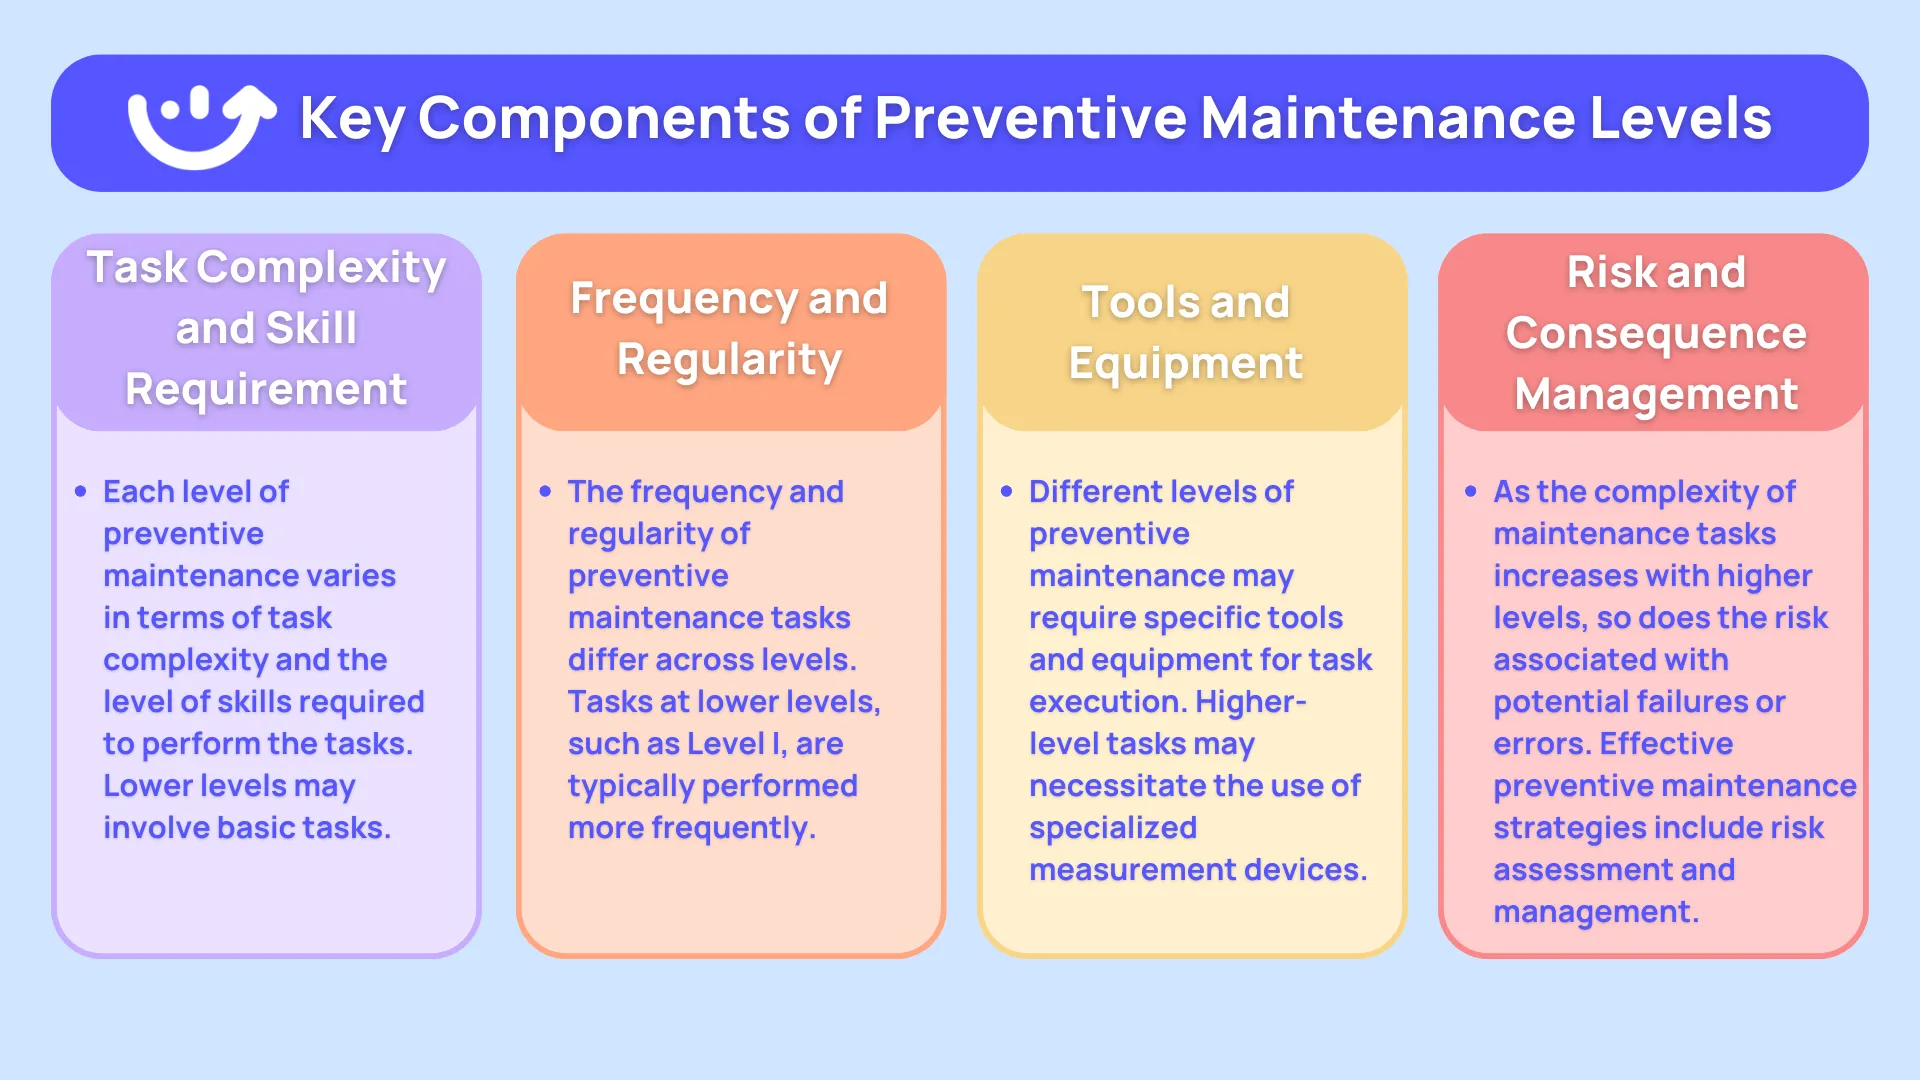
Any work done on equipment to lower the likelihood of failure counts as preventive maintenance. That description covers everything from a five-second visual check to vibration analysis with instrumentation. Here is the five-level breakdown of preventive work:
- Level I: Simple but essential upkeep performed safely with machine-integrated support equipment. Level one maintenance includes lubrication, condition monitoring, and filter clog removal, done on a regular cadence.
- Level II: Relatively simple procedures that still need a competent, trained person. Oiling moving parts, aligning pulleys or motors, and changing hard-to-reach air filters sit here.
- Level III: More involved work requiring skilled personnel who follow precise protocols. External measurement devices, invasive tasks, and technical parameter collection are level III.
- Level IV: Vibration and lubrication analysis, oscilloscope use, and infrared thermography. This is the ceiling of what competent on-site personnel usually handle. Vibration analysis is the classic level IV skill.
- Level V: Full disassembly with specialized knowledge and tooling that is usually only available from the manufacturer or an authorized service partner.
The multi-unit translation matters here. Preventive Level I in a restaurant is the closing team emptying and cleaning the fryer filter, wiping condenser coils on the reach-in, and logging the walk-in temperature. In a c-store it is the attendant checking the forecourt dispenser for leaks and damaged nozzles, clearing squeegee buckets, and logging cooler temps. Both of those live on a daily checklist, not on a work order queue.
Corrective Maintenance Levels
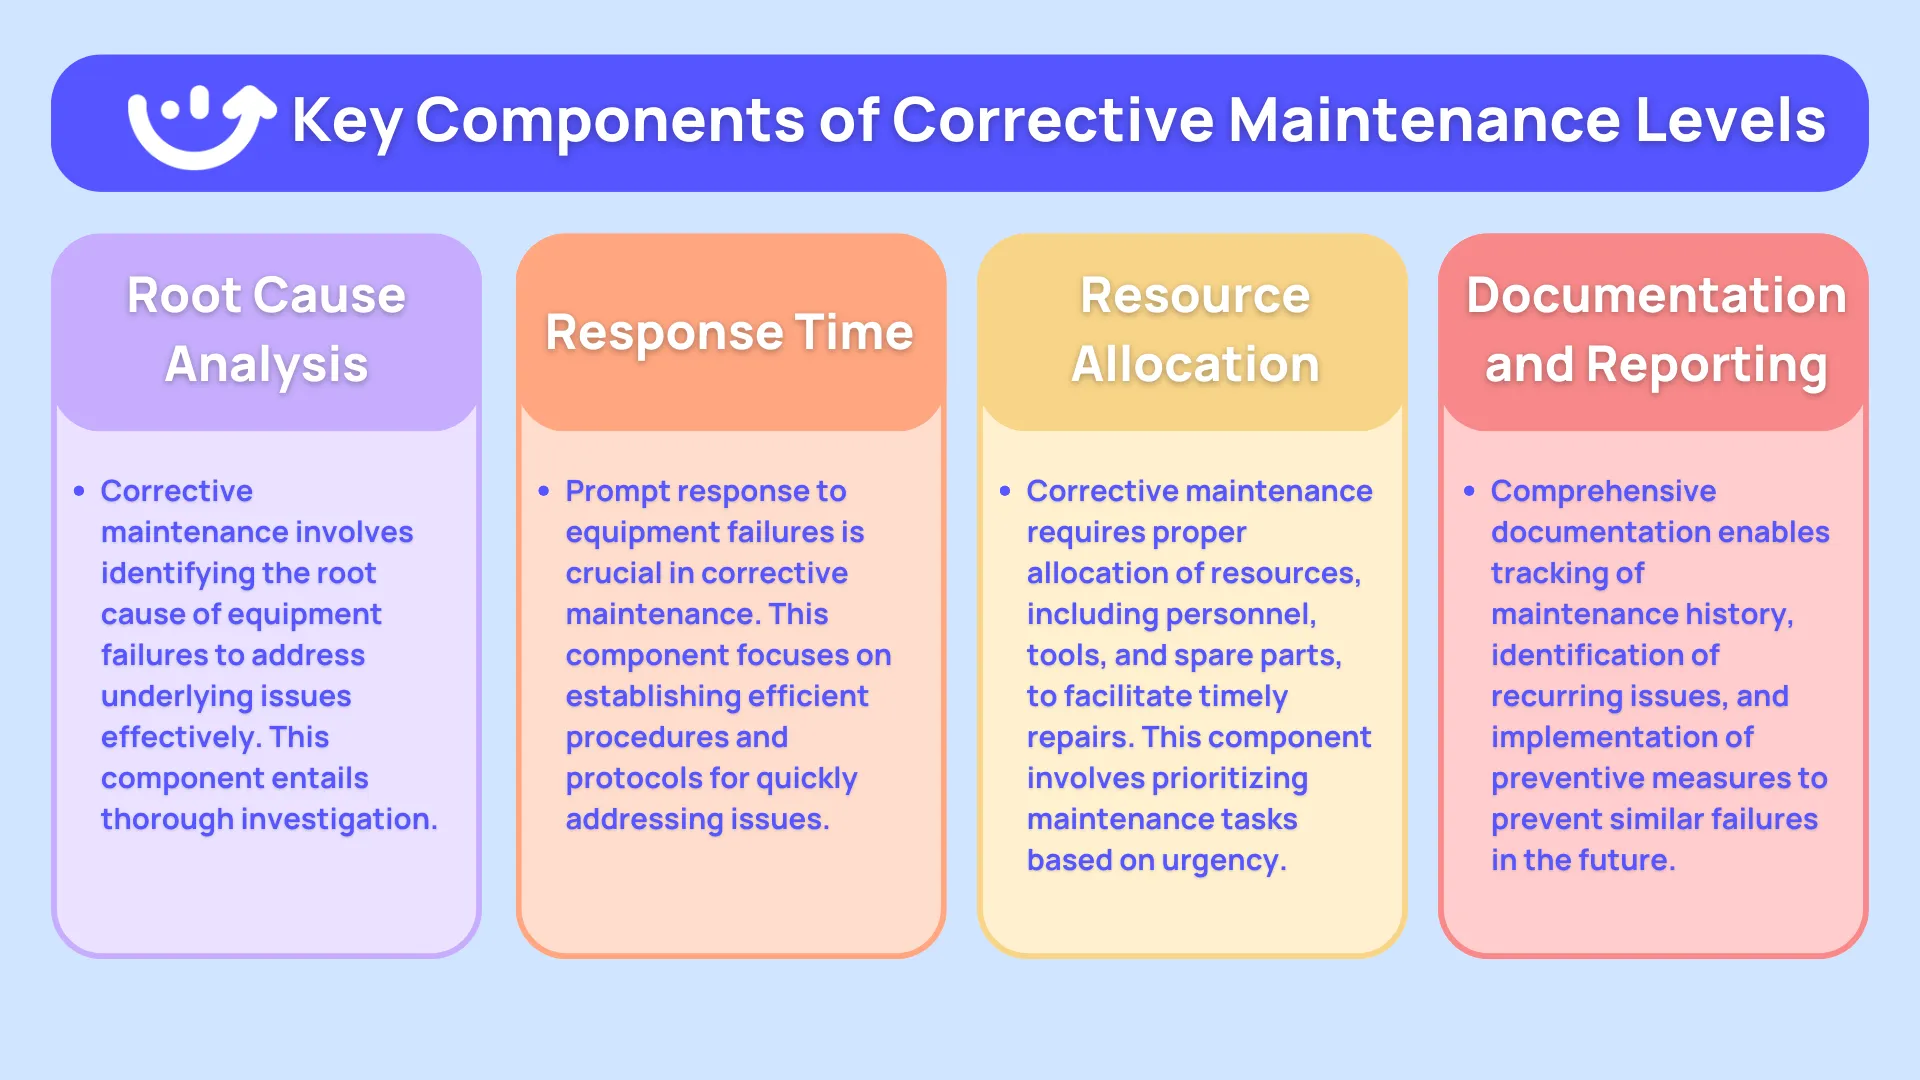
Corrective maintenance is any action needed to fix equipment and get it back to working order. Just as with preventive work, corrective maintenance levels climb in complexity and demand more specialist knowledge and tooling at each step:
- Level I: Replacing broken or worn parts on simple, readily accessible components. Changing a light bulb is the textbook example.
- Level II: Swapping air filters, fuses, belts, chains, slide rails, and rollers.
- Level III: Using diagnostic and measuring instruments, repairing refrigerant leaks, and replacing control cards, pumps, motors, and gears.
- Level IV: Repairs needing complex diagnostic equipment, such as pump modifications and compressor valve replacements.
- Level V: Comprehensive refurbishment, geometric or dimensional recovery, and advanced retrofitting.
Corrective Level I in a hotel is engineering swapping a burned-out corridor bulb and resetting a tripped GFCI in a guest bath. In retail it is an associate re-seating a loose shelf standard and replacing a fixture bulb. Everything above Level I becomes a ticket, which is why corrective maintenance work orders need a routing rule, not a hallway conversation.


Priced on per user or per location basis
Available on iOS, Android and Web


Level One Maintenance and CMMS
Simple interventions, essential and carried out on readily available components, constitute the first level of maintenance. These tasks can be performed by the operator or by individuals without specific training, without the need to open or disassemble the device. They require very few consumables or replacement parts, and when clear instructions are available on a handbook page or a screen, there is no specific danger to safety.
That last clause is where most operators get it wrong. The line between level one and level two is not difficulty. It is whether the person doing the work needs energy-isolation protection.
The safety boundary that decides what goes on a checklist
OSHA's lockout/tagout standard carves out a narrow exception for exactly the kind of work level one describes. Per 29 CFR 1910.147(a)(2)(ii):
"Minor tool changes and adjustments, and other minor servicing activities, which take place during normal production operations, are not covered by this standard if they are routine, repetitive, and integral to the use of the equipment for production, provided that the work is performed using alternative measures which provide effective protection."
All four conditions have to hold. Routine. Repetitive. Integral to production use. Performed with alternative measures that actually protect the worker. If any one fails, the exemption does not apply, full lockout/tagout is required, and it is not a task you hand to a shift lead on a checklist. The broader OSHA regulations that govern frontline equipment work sit behind that same logic.
The four-question test for any task your team wants to absorb:
- Can it be done without opening, disassembling, or reaching past a guard? If no, it is not level one.
- Is it routine and repetitive, done the same way every time, on a schedule? If no, it is not level one.
- Is it integral to normal production use rather than a repair? If no, it is not level one.
- Is there a written instruction the person can follow with no diagnosis and no judgment call? If no, it is not level one.
Level assignment is really a routing decision
Knowing a task is level 3 and not level 1 matters because it changes who gets the ticket. That is a routing problem, and it is what a modern work order system is actually for. The flow looks like this:
- An operator spots the issue during a daily checklist walk.
- The checklist item classifies it as level 1 fix-now or level 2 and above escalate.
- Level 1 work is completed in-line with a photo and a timestamp on the same checklist.
- Anything above level 1 becomes a work request instead of a completed task.
- The request auto-populates the asset, the location, and the category.
- A manager approves it and routes it by region, priority, and required skill.
- The assigned tech or vendor closes it out with photo evidence.
- The close-out writes back to the asset's service history so repeat failures are visible.
Matching interventions to their corresponding maintenance level is straightforward with a mobile-first platform like Xenia, which attaches checklists and specs directly to the asset record. Store staff or third-party vendors submit work requests via QR code with no login required. The form auto-populates the asset, location, and category. A manager approves and routes by region, priority, and skill, automatically. Approval, assignment, and routing all happen in the authenticated app, so the no-login path covers submission only. Tagging the asset is what makes this work at scale, which is why scan-to-create work orders from asset tags belong in the rollout plan, alongside a clear map of the types of work orders your locations actually generate.
The honest scope line
Be clear about what a frontline platform is and is not. Xenia is the submission and routing layer for level 1 and level 2 work at the location. It is not a depth CMMS. It does not match Limble or ServiceChannel for parts inventory, depreciation tracking, or vendor invoicing. If you need multi-warehouse spare parts costing, you need both, and the tradeoffs are laid out in work order software versus a full CMMS and in the definition of a computerized maintenance management system (CMMS). For context on adoption, Plant Engineering's maintenance research reports that 52% of industrial facilities run a CMMS and 59% use one to manage their preventive program. Most multi-unit brands have one. Very few have it in the hands of the people opening the store at 5am.
What are Maintenance Management Strategies?
A maintenance management strategy is the standing decision about how each asset gets cared for: on a calendar, on a sensor reading, on a risk score, or not until it breaks. Industrial plants, transportation networks, healthcare facilities, and commercial buildings all depend on one. Unanticipated failures cause interruption, lost revenue, and safety exposure in any sector where assets are fundamental to operations.
The numbers behind that risk moved sharply in the last two years, and the old 2019 figures no longer describe the market.
- Unplanned downtime now costs Fortune Global 500 companies roughly $1.4 trillion a year, about 11% of total revenue. Average plants run 25 unplanned downtime incidents a month, down from 42 in 2019, and lose 27 hours a month, down from 39. Incidents fell. Cost rose. (Siemens, The True Cost of Downtime 2024, analyzed by AEMT, with additional coverage at Automation.com)
- 71% of maintenance leaders call preventive maintenance a core strategy, but fewer than 35% actually spend the majority of their maintenance time on it. 58% still spend more than half their time reacting to breakdowns. Sample size 1,320 maintenance professionals across the US and Canada (MaintainX, 2025 State of Industrial Maintenance).
- 74% of facilities reported downtime stabilized or decreased, yet 31% saw downtime costs increase. Doing less reactive work is not the same as spending less on it.
For historical contrast, in Plant Engineering's 2019 Maintenance Report, 59% of engineers and managers still described maintenance as a cost center. Most operators now understand that maintenance is an investment required to keep equipment earning. Adopting a proactive maintenance strategy is how firms anticipate problems, limit unplanned downtime, and cut the odds of an expensive failure.
The multi-unit translation
Here is what every plant-focused article on this topic misses. Strategy at a plant means one asset register in one building. Strategy at 200 restaurants or 280 c-stores means 200 asset registers that have to behave like one. The hard part is not choosing a strategy. The hard part is executing the same strategy at every site with a rotating hourly workforce and no on-site technician.
That splits cleanly into two lanes. Daily checklists carry the level one work with photo and timestamp proof. QR work requests carry everything above it. Location hierarchy decides who sees what, so a DM sees their district and corporate sees all of it. Xenia's preventative maintenance scheduling and maintenance management tools are built around that split rather than around a technician-only work queue.
Aspen Management uses digital task management and real-time communication for property operations, which is the same pattern applied to a property portfolio instead of a store fleet.
6 Common Types of Maintenance Strategy
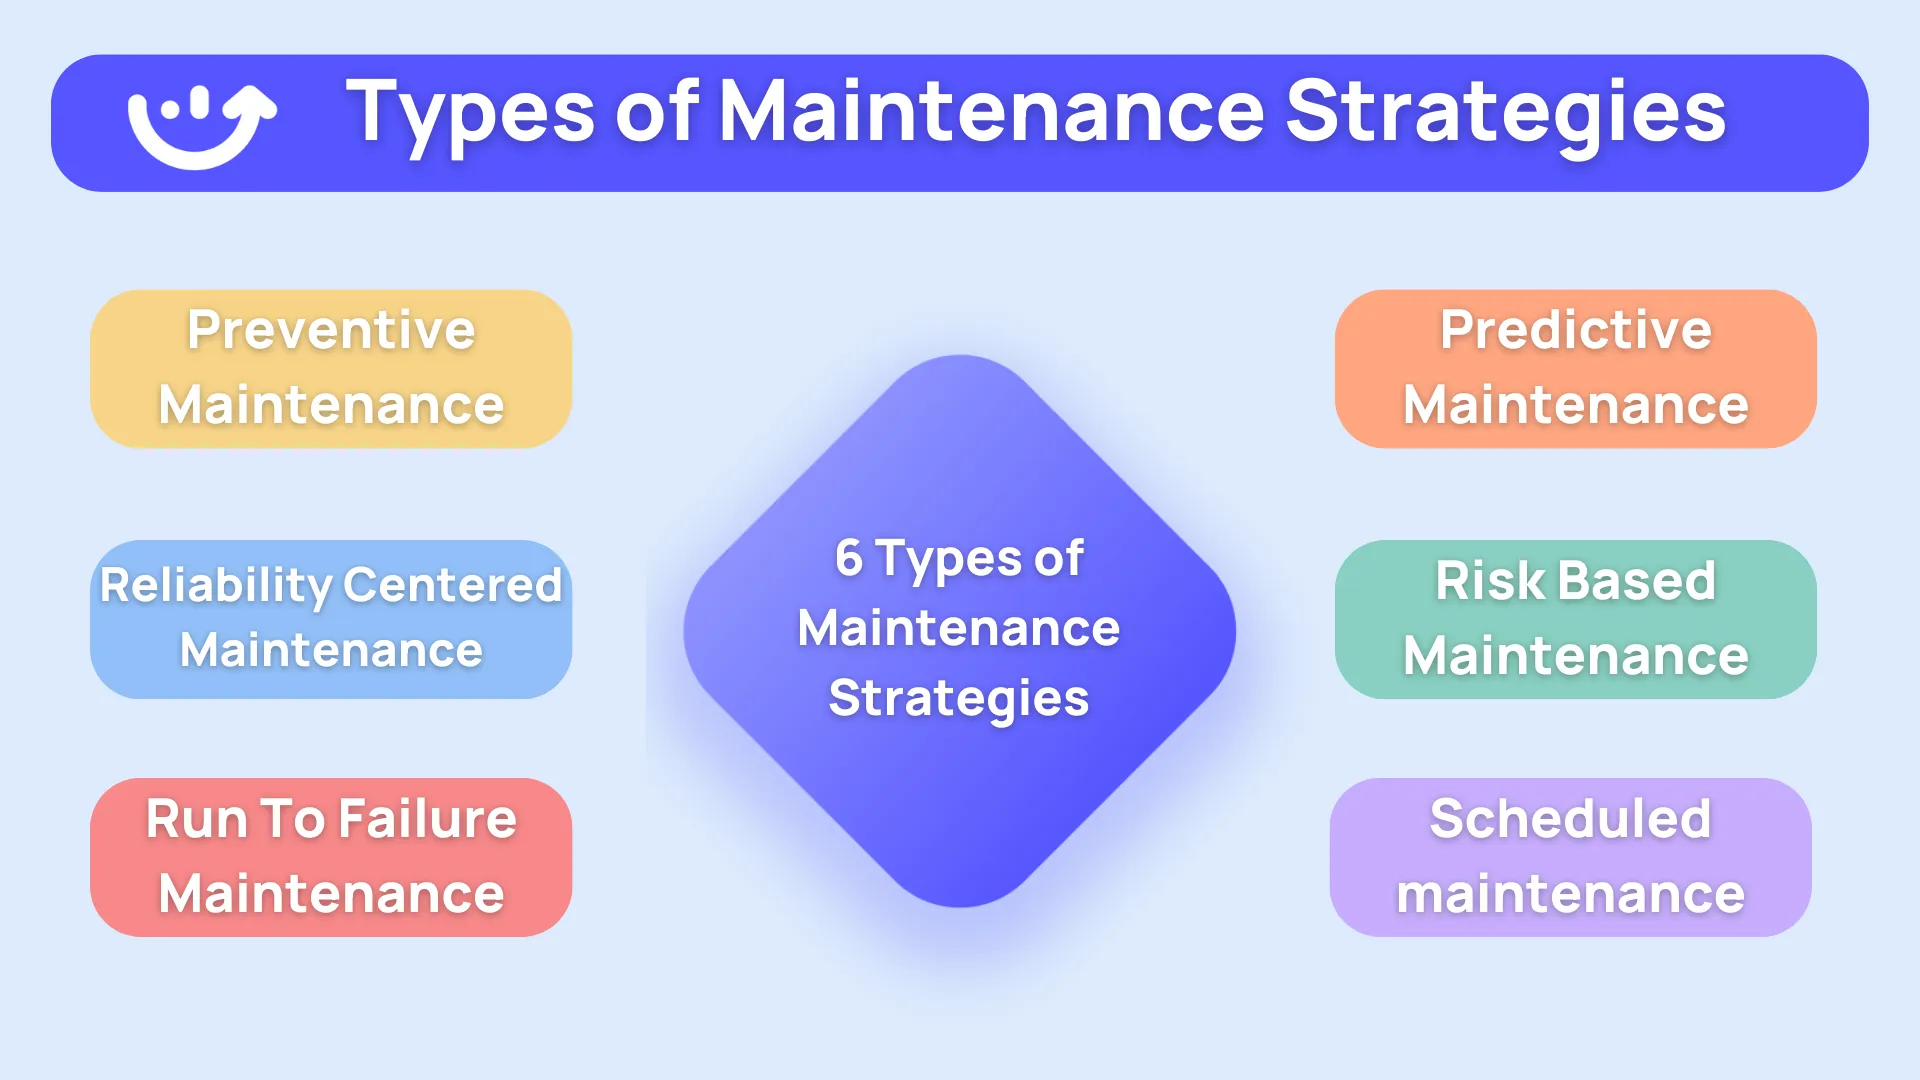
Six strategies cover almost every asset a multi-unit operator owns. The useful move is to connect each one back to the levels, because the strategy you pick determines the kind of work your locations generate and who has to do it.
| Strategy | Trigger | Typical maintenance level generated | Best for | Multi-unit failure mode |
|---|---|---|---|---|
| Preventive | Calendar or runtime interval | 1 to 2 | Safety-critical and high-use assets | Tasks get signed off without being done. Pencil-whipping. |
| Predictive | Sensor or condition data | 3 to 4 | Expensive assets with detectable degradation | Alerts fire at HQ and nobody at the store is assigned to act |
| Reliability-Centered | Failure-mode analysis per asset | 2 to 4 | Assets whose failure closes the location | Plan built once and never revisited as the fleet changes |
| Risk-Based | Consequence and likelihood scoring | 2 to 4 | Regulatory and safety-critical equipment | Risk scoring done at corporate and never reflected in store checklists |
| Run-to-Failure | Actual failure | 3 to 5 | Cheap, non-critical, easily replaced assets | Applied by accident to assets that were never assessed |
| Scheduled | Fixed calendar | 1 to 2 | Routine daily and weekly upkeep | No completion evidence, so no accountability |
In adoption terms, preventive leads at 71%, reactive and run-to-failure sit at 38%, and predictive trails at 27% (MaintainX 2025 State of Industrial Maintenance).
Preventative Maintenance Strategy
Preventative maintenance keeps assets in good working order by cleaning, adjusting, repairing, and replacing parts before they fail. It is the highest-volume strategy in a multi-unit fleet and it generates mostly level 1 and level 2 work, which is exactly why it belongs on store checklists rather than in a technician queue.
The multi-unit version: quarterly hood and grease-trap service across every kitchen in the group, on a fixed calendar, with a vendor sign-off photo attached to the asset record. The failure mode is pencil-whipping, where the task gets checked off without being done. Photo and timestamp evidence is the only cure. Setting a realistic preventive maintenance cadence per asset class beats one blanket schedule applied to a fryer, a dispenser, and a rooftop unit alike.
Predictive Maintenance Strategy
Predictive maintenance uses monitoring instruments and data analysis to catch degradation before failure. It generates level 3 and level 4 interventions, because interpreting a reading and acting on it requires a specialist. It is also the strategy with the widest gap between the alert and the fix.
In a restaurant or c-store fleet, the practical version is Bluetooth or LoRaWAN temperature monitoring on walk-ins and coolers, flagging compressor drift before the unit dies. One alert prevents a night of product loss and a health-code problem the next morning. Condition-based maintenance is the same idea applied to runtime and wear data. The trap is an alert that fires at HQ with nobody at store level assigned to act, which is why predictive maintenance work orders need a named owner and a clock.
Reliability-Centered Maintenance Strategy
Reliability-centered maintenance builds a bespoke plan for each asset based on how that asset actually fails. It is applied selectively, because the analysis costs real time. Expect it to generate level 2 to level 4 work.
Across locations, the selection rule is simple: the ice machine and the walk-in compressor get bespoke plans because their failure closes the store. The lobby TV does not. RCM makes each maintenance approach cost-effective by matching the plan to the failure mode rather than to the calendar. The multi-unit failure mode is a plan written once during a rollout and never revisited as the equipment fleet ages and new formats open.
Risk-Based Maintenance
Risk-based maintenance prioritizes assets by consequence and likelihood of failure, so the maintenance budget flows to whatever would hurt most. This approach is grounded in calculation, not preference, and it typically produces level 2 to level 4 work on the assets that score highest.
For multi-unit operators, fuel dispensers and hood suppression systems get first call on the budget because their failure is a safety and regulatory event, not an inconvenience. A cracked dispenser hose is a different category of problem than a flickering menu board. The failure mode is risk scoring done at corporate that never shows up in the store-level checklist, so the frontline still treats every asset the same. Work order prioritization is where that scoring has to land to matter.
Run-To-Failure Maintenance Strategy
In run-to-failure maintenance, an asset runs until it breaks and no preventive work is performed. It is legitimate only on non-critical equipment where spare parts are available, labor is reachable, and failure will not affect production or safety. It generates level 3 to level 5 corrective work, usually unplanned and usually at the worst time.
The honest version of this strategy is a $40 lobby lamp. Deliberate, documented, and correct. Run-to-failure works when it is a decision. It fails when it is a default that nobody ever approved. That distinction is the whole argument in run-to-failure maintenance operations, and it is why reactive maintenance work orders should be tracked as a percentage, not just as tickets.
Scheduled Maintenance
Calendar-based maintenance, as it is often called, reduces the frequency of equipment failures even though it cannot stop every catastrophic one. It generates level 1 and level 2 work and it is the most under-recognized strategy in the list, because the daily opening checklist is scheduled maintenance. Every unit. Every day.
Experts advise an 80/20 method based on the Pareto Principle, with 80% of maintenance work proactive and 20% reactive, even though no "perfect" level of reactive maintenance exists. A more current benchmark comes from Limble's planned versus unplanned maintenance ratio research, which found reactive organizations average 64% unplanned and 36% planned work, while high performers invert that to 36% unplanned and 64% planned. Fewer failures means lower maintenance and capital spend. The routine version of this lives on your restaurant opening checklist and your walk-in cooler temperature log, not in a maintenance module.
Maintenance Strategy Centralization and Alignment
Aligning maintenance strategy is what makes execution, scheduling, and budgeting possible, because common equipment types across comparable sites should be maintained to a common minimum standard. The first step is naming a single group accountable for coordinating maintenance across the business. Working through the phases of a planned maintenance program in that order produces five concrete advantages.
- Improved Efficiency
Consolidating maintenance work saves time and effort on comparable equipment, exposes where coverage is weakest, and focuses attention there. Duplicate work disappears, which lowers both labor hours and spend.
- Better Resource Allocation
Centralization improves how people, equipment, and supplies get distributed. Technicians move between assets and sites quickly because the approach and the standards are the same everywhere they go.
- Standardization of Processes
Standardization is a different thing from allocation, and it is the part most groups skip. It means one asset naming convention, one task library, one set of level definitions, and one escalation threshold, so a level 2 task means exactly the same thing at store 4 and at store 184. Without it, your data cannot be compared and your benchmarks are fiction.
- Improved Communication
A standard maintenance plan template gives departments and stakeholders a shared vocabulary, which speeds up handoffs and makes information sharing routine instead of heroic.
- Increased Safety
Centralized processes improve equipment integrity and reliability and lower the chance of accidents and injuries, because safety procedures get followed the same way at every location rather than reinvented per site.
What centralization actually means across 200 locations
Centralization in a plant means one department in one building. Across a fleet it means four specific agreements:
- One asset register with consistent tags. "Walk-in cooler" cannot be "WIC," "cooler 1," and "big fridge" at three different sites. Equipment management starts with naming.
- One definition of what a store may fix itself. Without it, one DM lets shift leads reset breakers and another routes every bulb to a vendor. Cost variance follows within a quarter.
- One escalation clock. A level 3 request at a rural site and an urban site should carry the same deadline, or an explicitly different one that somebody decided on purpose.
- One evidence standard. Photo at completion, timestamp, and assignee. Without all three, the completion record is unverifiable and your deferred maintenance backlog is invisible.
The volume involved is not trivial. ServiceChannel's restaurant facilities benchmark data covers more than 1.6 million work orders a year across more than 21,000 locations and 4,500 service providers. That is the scale a centralized program has to route without a human triaging every ticket, which is the practical case for multi-location work order management.
Permissions are the other half. DMs see only their district. Regional managers see all regions. Store managers see their store. One account, multiple scopes, no over-visibility and no data silos, which is how location hierarchy and scoped permissions are set up. G&M Oil replaced fragmented manual processes with Xenia across 220 stores, which is the literal definition of centralization and alignment at fleet scale.
Implementing An Effective Maintenance Strategy in 7 Steps
If you have never formalized maintenance before, building a strategy can look like a heavy lift. The work breaks into seven steps, which include assessing your current maintenance capability and managing the cultural change that comes with a new approach.
The sequence shifts a little by company size and asset mix, but every step matters if you want a plan precise enough to cut cost and raise output. One clarification before you start: these seven steps are a maintenance-strategy rollout sequence. They are not the seven steps of TPM autonomous maintenance, which is an operator-training program under the total productive maintenance umbrella. Same step count, different purpose.
Step 1: Identify Critical Assets and Current Maintenance Capabilities
Start by naming the assets that are vital to production and safety, then assess how mature your maintenance capability actually is. How established are your current systems and procedures, and are they serving the business or just existing?
The concrete output is a criticality-ranked asset list. Rank by three things: what closes the location, what creates a safety or health-code exposure, and what costs the most to replace. A walk-in compressor outranks a lobby TV on all three. As your team moves from reactive to proactive, the ability to fix things is only half the job. Planning, organization, and technical skill carry the rest.
Step 2: Analyze the Performance of Your Existing Operations
Before deciding what to change, take stock of how your maintenance operation performs today. Gather data on equipment availability, where downtime concentrates, why assets fail, spending patterns, and return on current effort. That is how you set maintenance goals that are both clear and relevant.
The concrete output is three baseline numbers captured before you change anything: planned versus unplanned work ratio, mean time to repair, and PM completion rate by location. Planned maintenance percentage is the single number executives understand fastest. Pick the rest of your reporting set from the standard maintenance KPIs and work order metrics, and make sure they align with your facilities, your business strategy, and your long-term goals.
Step 3: Decide on the Right Maintenance Approach for Your Assets
Choosing the correct approach per asset is what makes operations both safe and affordable. Criticality and condition should drive whether an asset gets a predictive, run-to-failure, or preventive plan. For critical assets, match the maintenance strategy to the specific failure mode so the total cost of failure stays low.
The concrete output is a per-asset strategy assignment using the comparison table above. Every asset gets exactly one strategy and exactly one named owner. If an asset has two strategies, it has none. If it has no owner, the strategy will not survive the first busy quarter.
Step 4: Develop a Clear Maintenance Plan
With strategies assigned, build the plan. It must specify when each task happens, how often, and what materials and tools are required. Detailed, plain instructions let crews do the work correctly and understand why it matters.
The concrete output is the level-1 cut. Go task by task and decide what goes on the daily checklist and what becomes a work request, applying the four-question test from the CMMS section above. This is the step most teams skip, and it is where cost variance between locations is born. A simple maintenance work order log is enough to hold the escalated half at the start, and a restaurant maintenance log works for single-vertical groups.
Step 5: Implement the Maintenance Plan
Next, the team puts the plan into action. Planning and scheduling means allocating resources, assigning responsibility, and confirming the work is actually happening. A disciplined project management approach avoids the usual setbacks. Training gets people on board and makes the change stick regardless of company size.
The concrete output is a pilot. Run 3 to 5 locations for 30 days before fleet rollout, and name the escalation path from store to DM to regional before day one. The practical mechanics of getting frontline teams to adopt a new system are covered in this guide to frontline operations platform rollout and adoption.
Step 6: Monitor Results and Improve Your Strategy
Collect data on asset performance to judge whether the approach is working. Maintenance analytics and benchmarking show you performance gaps, where time is going, and whether you picked the right strategy.
The concrete output is a review-by-exception routine. Review exceptions, not completion percentages. The dashboard that matters shows overdue corrective actions and repeat failures by asset, not a green completion bar that tells you nothing about risk. Watching how maintenance backlog management trends month over month is a better early warning than any single score.
Step 7: Develop a Feedback Loop
Spotting a weakness in the plan is one thing. Making sure your team consistently acts on it is harder and more valuable. Feed the results of your operational reviews back into the plan and adjust. Maintenance strategies should never be treated as permanent, because company needs and objectives move.
The concrete output is a standing monthly review with one rule: repeat work orders on the same asset either move that asset to a different strategy, or promote a recurring level 3 fix into a level 1 preventive task. If the same cooler gasket fails three times, the answer is not a faster tech. The answer is a gasket check on the weekly checklist.
Conclusion
Level one maintenance is not the least important work in your operation. It is the highest-volume work, and it is the only tier your store teams can absorb without adding headcount. Getting the level-1 cut right decides how many work orders you never have to open in the first place.
The practical sequence is short. Rank your assets by what closes the location. Run every candidate task through the four-question test. Put the level 1 work on a daily checklist with photo and timestamp proof. Route everything above level 1 as a work request with a named owner and a deadline. Review repeat failures monthly and promote the recurring ones back down to level 1.
Start with the calendar. The preventive maintenance calendar template gives you a ready-made cadence per asset class that you can adapt and push to every location this week, and the equipment maintenance log captures the service history behind it.
When you are ready to move the escalated half off text messages and paper, see how Xenia handles QR-code work requests and maintenance routing across locations, or book a demo and bring your own asset list.
Frequently Asked Questions
Got a question? Find our FAQs here. If your question hasn't been answered here, contact us.
How do you decide which maintenance tasks your store team can do?

What is organizational-level maintenance?
What is the difference between level one maintenance and preventive maintenance?
Who can perform level one maintenance?
What are the 5 levels of maintenance?
What is level one maintenance?
A Modern, AI-Powered Platform Built for Facility Operations
Xenia connects maintenance, safety, inspections, and daily operations into one mobile-first platform. Facility teams respond faster, prevent downtime, and maintain compliance, while leadership tracks performance across all buildings in real time.
Why Facility Managers Choose Xenia:
🤖 AI-Powered Inspections, Verify safety equipment and compliance automatically with AI photo analysis. Surface critical maintenance issues instantly with AI-powered summaries.
🛠️ Work Orders & Maintenance, Report issues via mobile or QR codes. Route requests to teams or vendors. Schedule preventive maintenance for HVAC, elevators, and emergency systems to reduce downtime.
📊 Safety & Visibility, Deploy fire safety and hazard inspection workflows. Monitor work order resolution times and asset health across all facilities.
Manage work orders, maintenance, and safety inspections across all facilities from one platform.